
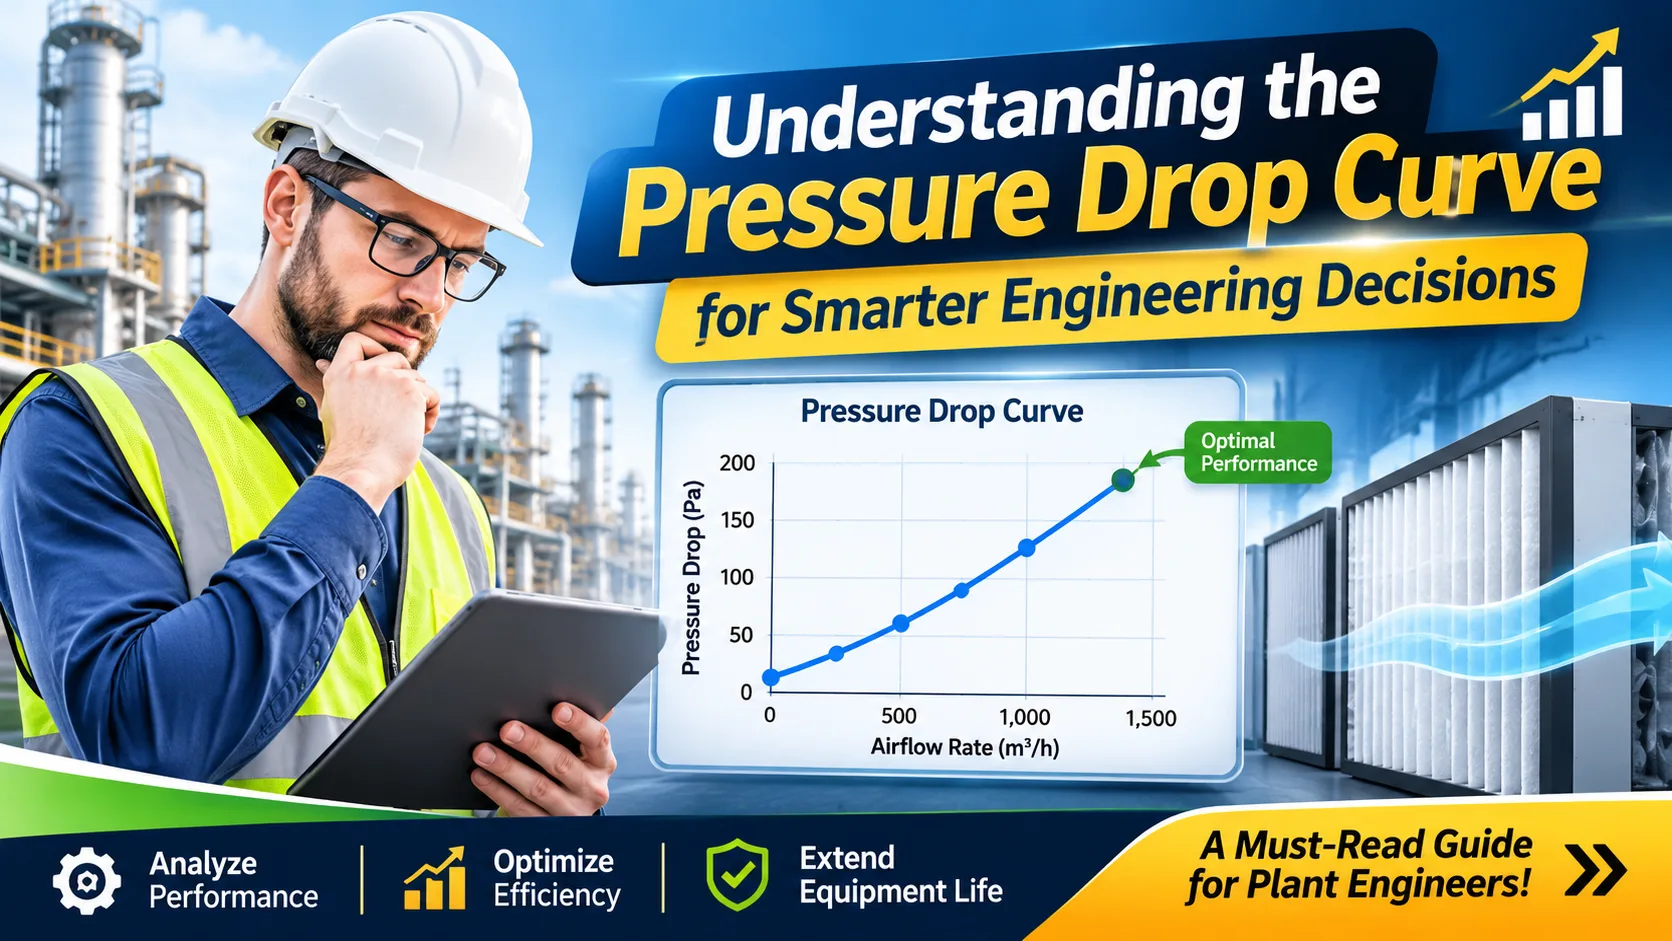
For plant engineers, a filter's pressure-drop curve is more useful than a single pressure-drop figure. It shows how resistance changes as airflow increases and provides a practical way to evaluate whether a filter is correctly
sized for the operating point.
This matters across industrial HVAC, gas turbine intake systems and liquid-aerosol applications where excessive resistance can reduce available airflow and increase fan or intake-system loading.
Understanding the curve also helps engineers make better decisions about filter changeout rather than replacing elements based only on a calendar interval.
What Does a Filter Pressure-Drop Curve Show?
Pressure drop is the difference in pressure measured across the filter between the upstream and downstream sides.
A typical curve plots:
Airflow or face velocity on the horizontal axis
Pressure drop on the vertical axis
As airflow increases, pressure drop generally increases. The exact relationship depends on the filter construction, media, available filter area and operating conditions.
For example, a coalescer panel may use a larger effective media area to manage moisture and liquid aerosols while maintaining relatively low resistance at the intended airflow. Airguard's CP2-
AG, for example, is specified as a V-pleated coalescer panel with a stated face velocity of 9 m/s and is designed for applications including gas turbine intakes and offshore environments.
The curve should therefore be read at the actual operating point, not at an arbitrary airflow value.
Initial Pressure Drop vs Loaded Pressure Drop
One of the most common mistakes in filter selection is treating initial pressure drop as the complete operating picture.
A clean filter produces an initial pressure drop. As contaminants accumulate, the filter's resistance can increase.
The engineering distinction is:
Condition | What it tells the engineer | |
|---|---|---|
Initial pressure drop | Resistance when the filter is clean | |
Operating pressure drop | Resistance under current conditions | |
Loaded pressure drop | Resistance after contaminant accumulation | |
Changeout pressure | Point at which replacement may be required |
For a gas turbine or industrial ventilation system, this progression matters because the available pressure margin can change throughout the filter's service period.
A filter that appears suitable when clean may become restrictive after significant loading.
How to Read the Curve at the Operating Point
Start with the actual airflow through the filter bank.
If the system handles 100,000 m³/h and contains multiple filters operating in parallel, the airflow through each filter is not 100,000 m³/h. The approximate per-filter airflow depends on the number of active elements and the flow distribution.
Once the airflow per filter is established, locate that value on the pressure-drop curve.
Then move vertically until it intersects the curve and read the corresponding pressure drop.
The result should be compared with the system's allowable resistance.
This simple process helps prevent a common sizing error: selecting a filter based on its maximum published airflow without checking its resistance at the plant's actual operating point.
Face Velocity Changes the Pressure-Drop Picture
Face velocity is another important variable.
It can be calculated as:
Face velocity = Airflow ÷ Effective filter face area
Increasing the available filter area reduces the airflow passing through each unit area of media.
That can influence pressure drop, contaminant loading and service life.
This is particularly relevant when comparing filters with the same nominal dimensions but different internal constructions. A pleated or pocketed design may provide substantially more effective media area than a flat panel occupying the same face dimensions.
For EPC and plant-maintenance teams, the comparison should therefore include filter area, not just width, height and depth.
Coalescer Filters Require Additional Consideration
Coalescer filters are used where moisture, liquid aerosols or other droplets need to be managed as part of the intake or ventilation system.
Their pressure-drop behaviour needs to be considered alongside the contaminant being removed.
Moisture and particulate can interact. Under some operating conditions, captured material can increase resistance faster than expected. Parker's filtration guidance notes that coalescing systems require attention to differential pressure and that excessive contamination can contribute to premature clogging.
For gas turbine intake systems, this becomes especially important in wet, coastal or offshore environments.
A coalescer may be used upstream of other filtration stages to manage moisture and aerosols before air reaches downstream filters. Parker also notes that coalescing filtration can be used to agglomerate droplets and help prevent captured dust from becoming excessively wet and increasing pressure drop.
The pressure-drop curve should therefore be considered together with the contaminant-loading profile.
Pressure Drop and Gas Turbine Filters
Gas turbine filters operate at high airflow rates, so relatively small differences in resistance can become significant across a large filter bank.
Engineers should evaluate:
Design airflow
Number of filters
Face velocity
Initial pressure drop
Expected loading
Maximum allowable resistance
Filter efficiency
Environmental exposure
Parker's Altair filtration documentation illustrates why pressure loss is a key comparison parameter, with different filter configurations offering different efficiency and pressure-loss characteristics.
This is why selecting a gas turbine filter purely from an efficiency rating can be misleading.
The filter needs to deliver the required particle removal while remaining within the intake system's pressure-loss envelope.
Using Pressure Drop to Plan Filter Changeout
Pressure-drop monitoring can also provide a more defensible approach to filter replacement.
Rather than replacing every filter after a fixed number of months, maintenance teams can monitor differential pressure and establish a site-specific changeout point.
The practical approach is:
Record the clean-filter pressure drop.
Establish normal operating airflow.
Monitor differential pressure during operation.
Track the rate of pressure increase.
Define the allowable pressure-drop limit.
Schedule replacement before the system reaches an unacceptable condition.
The actual changeout limit should come from the equipment manufacturer's requirements, filter specification and site operating conditions.
For coalescing systems, maintenance guidance may also include inspection and drainage requirements depending on the equipment configuration.
What Engineers Should Check Before Approving a Filter
A pressure-drop curve should never be reviewed in isolation.
Before approving a replacement, verify:
Filter dimensions
Effective media area
Design airflow
Face velocity
Initial pressure drop
Applicable loaded-pressure information
Filtration efficiency
Filter construction
Sealing arrangement
Operating environment
Contaminant characteristics
For replacement or OEM-equivalent applications, the original filter reference can be useful, but technical characteristics should still be confirmed.
A supplier's published pressure-drop curve is most useful when the test conditions and airflow basis are clearly understood.
Practical Pressure-Drop Review
When reviewing a filter quotation, engineers can use a simple comparison:
Parameter | Existing requirement | Proposed filter |
|---|---|---|
Airflow | Plant design value | Confirm |
Face velocity | System limit | Confirm |
Initial pressure drop | Design allowance | Compare |
Efficiency | Required level | Confirm |
Media area | Existing configuration | Compare |
Loaded resistance | Changeout basis | Review |
Environment | Dust/moisture/salt | Confirm |
Filter changeout | Site limit | Establish |
This approach gives maintenance and procurement teams a common technical basis for comparing alternatives.
Conclusion
A pressure-drop curve is not simply a graph included in a filter datasheet. It is a practical engineering tool for understanding how a filter will behave at a defined airflow and how resistance may change as the element loads.
For coalescer filters, moisture and aerosol loading should be considered alongside pressure drop. For gas turbine filters, airflow, efficiency, environmental conditions and intake-system pressure limits all need to be considered together.
When evaluating replacement filtration, engineers can also review specialist coalescer panel filters to compare available constructions and application-specific options.
The most reliable filter selection process is therefore based on the complete operating point, not a single pressure-drop number.
FAQs
1. What is filter pressure drop?
Filter pressure drop is the difference in air pressure measured before and after a filter. It indicates the resistance the filter creates against airflow.
2. Why does filter pressure drop increase over time?
As dust, moisture, oil or other contaminants accumulate on the media, airflow resistance increases. This creates a higher loaded pressure drop.
3. How does face velocity affect pressure drop?
Higher face velocity generally increases pressure drop because more air is forced through the same filter area. Correct sizing helps control resistance.
4. When should a filter be changed based on pressure drop?
Changeout should follow the equipment manufacturer's specified differential-pressure limit and the filter's operating requirements rather than a fixed calendar interval.
5. Why is pressure drop important for coalescer filters?
A coalescer must remove liquid aerosols while maintaining acceptable airflow resistance. Excessive loading can increase pressure drop and restrict system airflow.